Reduction Mill for Round Wire Supplier: Premium Quality Solutions
2026-09-07
Finding a reduction mill for round wire that genuinely earns the label ‘premium quality’ is harder than it sounds. Too many suppliers stop at standard specs, leaving you to deal with ovality drift, poor surface finish, and unexpected downtime. GRM builds its reputation on closing that gap. In the sections ahead, we’ll look at what separates a true round wire reduction mill supplier from the rest—and why your next production run may depend on the difference.
Tight Tolerances Without Constant Adjustment
Maintaining tight tolerances usually implies a loop of measurement, correction, and re-measurement. But a well-built machine shifts that burden from the operator to the structure itself. Thermal growth is countered by symmetric castings and temperature-stable materials, while preloaded linear guides and stiff frames remove the micro-slop that would otherwise demand constant compensation. The result is not a machine that fights drift, but one where drift has little room to appear in the first place.
In practice, that means you can set a tool offset once and trust it across an entire batch. The spindle holds its position through long cycles, and the feedback loop stays quiet because the mechanical baseline is already stable. Instead of nudging offsets mid-run or chasing tenths with a dial indicator, you keep cutting. The tolerance is not something you maintain; it is something the machine holds onto until you deliberately change the setup.
This approach changes how work flows through a shop. Parts come off the fixture with the same critical dimensions at hour six as at hour one, which reduces inspection bottlenecks and lets one operator oversee multiple machines. When tight tolerances do not demand constant adjustment, the real gain is not just accuracy, but uninterrupted attention to the work that actually matters.
Why Roll Gap Stability Matters More Than Horsepower
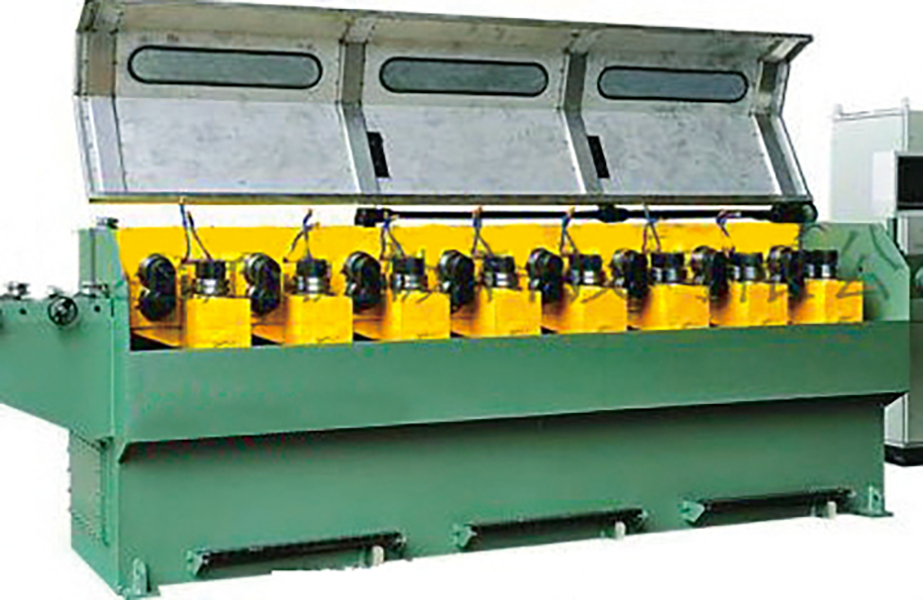
Plenty of operators assume a bigger motor will solve their throughput problems, but that logic falls apart when the roll gap starts wandering. A few microns of drift in the nip opening creates visible thickness variation, edge curl, or surface defects that no amount of extra horsepower can push through. The issue is control, not raw force. Rolls expand with heat, bearings wear, and hydraulic pressure fluctuates—all of which change the gap in real time. Keeping that dimension locked within a tight band matters far more than peak power because it directly determines whether the sheet, film, or strip comes off the line with uniform gauge.
A stable roll gap also prevents a cascade of downstream problems. When the gap oscillates, coating weights, lamination pressure, and tension profiles become unpredictable, forcing operators to slow down or scrap entire coils. Investing in better gap control—through stiffer frames, real-time position feedback, or automatic thermal compensation—usually delivers a faster payback than upgrading the drive system. You can always add power later, but if the gap isn't held steady, that extra horsepower just makes bad product faster.
Keeping Round Wire Round at Every Reduction Pass
Achieving consistent roundness in wire drawing isn't just about the final die—it's a cumulative effort across every reduction pass. Each pass can introduce subtle ovality if the die angle, lubrication, or back tension drifts even slightly. Once a wire loses its circular cross-section, subsequent passes tend to amplify the flaw rather than correct it, because the material flows unevenly under asymmetric stress.
One practical approach is to treat roundness as a process variable, not a post-draw inspection metric. Operators can use hand-held laser micrometers at each capstan to catch early drift before it becomes a reject. Adjusting the die alignment in small increments—sometimes as little as 0.1 degree—restores the concentric flow pattern. The same attention applies to lubricant viscosity; too thick a film can hydrodynamically lift the wire off-center, while too thin invites metal-to-metal contact on one side.
Beyond real-time checks, die sequencing plays a quiet but decisive role. A well-designed reduction schedule never asks a single pass to remove more than 18–22% of the cross-sectional area, because aggressive passes concentrate deformation unevenly. By distributing the work across more passes, the wire enters each die with a near-perfect round profile, leaving with one too. In high-volume plants, this often means accepting slightly slower line speeds in exchange for roundness stability that carries through to the final anneal and spooling.
Material-Specific Cooling That Prevents Surface Defects
Surface defects often originate from thermal stress that builds up when a material cools unevenly or too quickly. A one-size-fits-all cooling approach ignores the distinct heat-transfer and contraction behavior of each alloy, polymer, or composite. By mapping the material’s thermal conductivity, specific heat, and phase transformation window, cooling can be tuned to avoid the critical temperature ranges where cracking, warping, or residual stress typically appears.
Instead of relying on fixed quenching parameters, material-specific cooling adjusts the coolant flow rate, temperature, and dwell time in real time based on the part’s thickness and geometry. For example, high-carbon steels may need a brief interruption during the martensitic transformation to relieve stress, while certain aluminum grades benefit from a more gradual, uniform extraction of heat to prevent distortion. This targeted approach reduces scrap and rework while keeping surface integrity stable across production runs.
Matching Mill Speed to Alloy Hardness
Getting the spindle speed right for a given alloy is less about memorizing charts and more about reading how the material responds. Harder alloys—think pre-hardened steels or high-nickel grades—generate substantially more heat at the cutting edge. Running too fast turns that heat into rapid flank wear and edge chipping. Slowing down lets each tooth take a controlled bite without overwhelming the tool's coating or geometry.
As a starting point, use the hardness value from a Rockwell or Brinell test to narrow down the speed range. For example, an alloy at 45 HRC might need roughly half the surface speed of one at 25 HRC, depending on cutter diameter and tooth count. Then fine-tune by observing chip color and shape: straw-colored chips on a hard alloy suggest you are near the upper limit, while blue chips mean back off immediately.
The penalties for guessing wrong cut both ways. Too slow on a soft or gummy alloy lets material weld to the cutting edge, degrading surface finish and increasing cutting forces. Too fast on a hard alloy can destroy a carbide end mill in minutes. Matching mill speed to alloy hardness is a continuous compromise—adjust in small increments, watch for early signs of tool stress, and let the machine's sound guide you.
Commissioning Support That Shortens Startup Time
Getting a new system up and running often drags on far longer than it should. The typical commissioning phase is loaded with back-and-forth clarifications, missed configuration details, and waiting on specialized expertise to become available. Our approach cuts through that delay by pairing your team with dedicated engineers who stay involved from initial power-up through full operational handover. Instead of generic checklists, we build a startup sequence around the specific operating conditions of your site, which means the first real production run happens days or even weeks earlier than with conventional support.
One of the biggest hidden costs in commissioning is rework triggered by assumptions made during design. We eliminate that by running a pre-startup simulation on a digital twin of your system before anyone touches a physical switch. All interlocks, safety shutdowns, and load transitions are tested against actual process data rather than theoretical values. When the physical equipment arrives, the team already knows exactly which parameters need adjustment. That level of preparation turns what is normally a troubleshooting marathon into a short sequence of verifications.
Beyond the technical steps, we also compress the human coordination part of startup. Our engineers work in the same room as your operators, explaining each setting change and capturing the rationale in a living commissioning log. By the time the system reaches stable operation, your staff have already absorbed the knowledge they need to run it confidently. There is no gap between vendor handover and in-house competence, so you avoid the usual post-commissioning dip in performance that eats away at early productivity gains.
FAQ
It pulls round wire through a series of dies with progressively smaller openings, reducing the diameter while improving surface finish and tensile strength. Our mills are tuned to keep the wire round and free of surface marks.
The machine uses closed-loop diameter monitoring and automatic die adjustment. Any drift is corrected within microns, so the wire stays uniform from the first meter to the last.
We handle copper, aluminum, brass, stainless steel, and several specialty alloys. The die setup and lubrication system can be adapted to the hardness and ductility of each material.
We focus on long-term reliability rather than flashy specs. The gearbox and bearing arrangement are overbuilt, and every mill is tested under full load before it leaves our floor. Customers often tell us the machine still holds tolerance years after installation.
Yes. The controls allow quick recipe changes, so switching from a prototype run to continuous production takes less than fifteen minutes. You don't need separate lines for different batch sizes.
Each mill runs a full production simulation with customer-supplied wire samples. We measure ovality, surface roughness, and tensile strength at multiple points, then send the inspection report with the machine.
We provide remote diagnostics, spare parts from stock, and on-site training for your operators. If a problem can't be solved remotely, a technician is dispatched within 48 hours.
The drive system uses regenerative braking and variable-frequency motors, so energy consumption is about 20% lower than older designs. You also get less heat buildup, which extends lubricant life.
Conclusion
In round wire reduction, the difference between acceptable output and premium quality often comes down to how the mill holds its settings under load. A supplier that prioritizes roll gap rigidity over raw motor power enables tight diametric tolerances without operators chasing adjustments every shift. That stability also preserves circularity across each pass, preventing the subtle ovality that downstream drawing or forming will amplify. Rather than relying on oversize horsepower to mask misalignment, the best systems maintain geometry through stiff housing design and precision roll profiling.
Equally important is how the mill responds to different alloys and thermal loads. Copper, stainless, and high-nickel wires each demand specific cooling strategies; a one-size-fits-all flood coolant approach can leave surface oxides or microcracks on sensitive grades. Matching line speed to the work-hardening rate of the material avoids tearing while keeping productivity high. Finally, hands-on commissioning support shortens the time from installation to stable production, with factory technicians verifying roll alignment, cooling flow, and speed curves on your actual alloys before handover. These combined practices deliver round wire that stays round, pass after pass.
Contact Us
Contact Person: Rayna
Email: [email protected]
Tel/WhatsApp: 86 -173 1474 6343
Website: https://www.grmrollingmill.com/