Radial Artery Compression Device Factory: Precision Manufacturing for Cardiac Patient Safety
2026-09-18
When a cardiac procedure ends, the real test begins—keeping the radial artery puncture site safe without adding to patient stress. That’s where precision manufacturing stops being a buzzword and becomes a lifeline. At INT, every compression device leaving our factory is built with one goal: consistent, gentle hemostasis that cardiac patients can trust. But how exactly does factory-level precision shape recovery? Read on to see the hidden engineering behind safer cath lab outcomes.
Micron-Level Molding for a Fragile Radial Artery
Molding at the micron scale for a vessel as delicate as the radial artery demands a completely different mindset from standard polymer processing. The wall thickness here is often under two hundred microns, and the lumen must stay perfectly round under physiological pressure without kinking or collapsing. We start with a proprietary low-temperature curing silicone that flows like water at injection, yet retains enough green strength to be demolded without tearing. The mold itself is machined to a surface roughness below Ra 0.05 µm, and every cavity is optically inspected before each run. Because the artery flexes continuously in the wrist, we bias the parting line away from high-strain zones and use a three-stage pressure profile that prevents micro-voids near the transition from straight to tapering sections. Operators handle the parts only with vacuum tweezers, and final inspection is done under 50× magnification with a go/no-go mandrel rather than contact gauges.
What makes this feasible in production is not the molding machine itself, but the tooling strategy and material pairing. Instead of a traditional sprue and runner, we use a heated micro-nozzle that deposits a 0.4 mm diameter shot directly into the gate, eliminating cold slugs and reducing shear heating. The silicone is filled with a low aspect ratio fumed silica at 12% by weight, which gives a thixotropic index of 2.1 — thin enough to fill the thinnest wall features, but thick enough to hold the crown of the lumen without slumping. Mold temperature is held at 38 °C ± 0.5 °C, which is below the silicone's gel point but high enough to prevent condensation on the core pins. Cycle time is 90 seconds, but the real bottleneck is post-cure conditioning: each part sits in a humidity-controlled chamber at 60% RH for 24 hours to stabilize the surface energy before coating.
Handling the fragile part after ejection is where most attempts fail. The radial artery model has a natural curve with a radius of 28 mm, and straightening it even temporarily introduces micro-cracks at the intima-media interface. We designed a custom nest that supports the part in its as-molded geometry, with a soft Shore 00-30 elastomer cushion that absorbs the shock of robot transfer. From mold opening to packaging, the part is never exposed to a pulling force above 0.3 N, and no metal tool ever touches the molded surface. Packing is done in a nitrogen-purged tray with individual pockets lined with a non-shedding, antistatic film. This level of care sounds excessive, but the failure mode in the field is not visible to the naked eye — a sub-20 µm crack at the inner radius that opens only after 50,000 cycles of simulated wrist flexion. Catching that at the micron level before it leaves the cleanroom is the difference between a model that trains surgeons well and one that fails halfway through a procedure.
The Sterile Zone Where Precision Meets Patient Safety
Inside an operating suite, the sterile zone operates as a quiet anchor. It begins with strict hand preparation and extends outward through gowns, gloves, drapes, and the disciplined movement of every team member. A single lapse—an ungloved hand passing over an open tray, a mask worn loose, a door left ajar—can compromise the entire field. Precision here is not about speed; it’s about consistency. Each instrument is placed within easy reach, each surface is treated as a potential carrier, and each person knows exactly where their body may move without breaking the invisible seal.
What makes this zone reliable is less the equipment and more the shared vigilance. Staff double-check each other’s technique without ceremony, because in that space, silence can be a safeguard. Airflow systems are configured to push particles away from the patient, but human habit remains the strongest barrier. When a circulator hands off a package, the transfer follows a choreographed path that never crosses the sterile boundary. That precision lowers the risk of surgical site infections and protects the patient from threats that are invisible until they become complications.
Patient safety, in this context, is not an abstract goal. It lives in the moment a scrub nurse refuses to accept a tray with a torn wrapper, or when a surgeon pauses to adjust a light rather than reach across the field. The zone holds because every person treats the rules as non-negotiable. In that quiet discipline, precision and safety become the same act.
From Extrusion to Packaging: A No-Shortcuts Build
The raw polymer enters the extruder at a controlled rate, and we don't rush that first melt. Temperature zones are tuned by hand, not left to a preset curve, because every batch behaves slightly differently. If the melt pressure spikes by even half a bar, the line stops, the material is purged, and the barrel gets a visual inspection before we restart. That's the kind of slowdown most factories avoid, but it's exactly where the integrity of the finished part begins.
After the profile leaves the die, it passes through a cooling bath where the water temperature is checked every thirty minutes, not just recorded on a log. Operators run a fingernail along the surface to catch any micro-tears that sensors would miss. Then the cutting station trims each length to a tolerance tighter than the industry standard, and every tenth piece goes to a jig for a dimensional check. No one is looking at a clock here; they're looking at the material.
When it finally reaches packaging, each item is wiped down with a lint-free cloth, not because it's visibly dirty, but because static attracts dust that ruins adhesion later. The wrapping itself is a heavy-gauge, anti-abrasion film, and the corners get extra padding before the box is sealed. The last step is a handwritten tag with the batch number and the name of the inspector who signed off. That signature means someone actually walked the whole line, from raw pellet to taped carton, and refused to cut any corners.
Why Our Pressure Curve Mimics a Nurse's Touch
Most automated devices inflate in a straight, robotic line — quick, uniform, and entirely unlike human hands. We spent months mapping the subtle variations of a skilled nurse's palpation: the initial gentle rise, the brief pause to find the pulse, then the gradual release that avoids startling the patient. Our pressure curve follows that same rhythm, easing into the arm instead of clamping down.
That curved approach does more than feel familiar. It lets the sensor catch faint oscillations that a rigid ramp often misses, especially in patients with weak peripheral pulses or thicker tissue. By mimicking the nurse's touch, the cuff communicates with the artery rather than overpowering it — leading to readings that hold up in real clinical settings, not just in ideal lab conditions.
The result is a measurement sequence that feels less like a machine and more like a careful pair of hands. Patients relax sooner, movement artifacts drop, and the numbers reflect what a trained clinician would actually measure. It's a small shift in engineering that closes the gap between automation and attentive care.
Fail-Safe Testing That Flags Any Leak Before Shipment
Every unit rolls through a gauntlet of pressure decay, mass flow, and helium sniffer checks that can spot seepage down to a whisper of a bubble per minute. The rig doesn't just pass or fail — it logs the exact leak rate, location, and trend so questionable parts never make it to the pallet.
Our test benches are calibrated against NIST-traceable masters every shift, and the software runs a self-diagnostic before each cycle. If a fitting is slightly loose or a seal starts to fatigue, the system flags it before it becomes a field failure.
Only after a part survives the full profile — including thermal cycling while under pressure — does it earn a shipping label. No exceptions, no overrides, no 'probably fine' calls.
Every Device Carries a Digital Passport to the Cath Lab
The moment a catheter, stent, or guidewire enters the cath lab, its entire history can now travel with it. Each device receives a unique digital identifier at the point of manufacture—a kind of passport that records batch numbers, sterilization cycles, expiration dates, and even the exact materials used. This isn't just a barcode on a box; it's a living record that follows the device from the loading dock to the sterile field, updating with every scan.
For clinicians, this means no more second-guessing whether a balloon catheter has been recalled or if a particular lot is still within its safe-use window. A quick scan ties the device directly to the patient's electronic record, creating an unbroken chain of custody. If a problem surfaces later, the team can trace the device back to its origin in seconds—not days—and pull affected stock before it reaches another patient.
Beyond safety, the digital passport quietly reshapes inventory management. Cath labs deal with hundreds of high-cost consumables, many of which are used once and discarded. Knowing exactly what is on the shelf, what has expired, and what was used during a procedure eliminates waste and prevents the frantic search for a compatible stent. The passport doesn't just identify a device; it turns every item into a source of actionable data.
FAQ
It combines precision tooling with cleanroom assembly and real-time force calibration so every device delivers consistent hemostatic pressure without compromising distal blood flow.
Each unit passes through automated pressure-mapping stations that test band tension, air bladder inflation, and release valves against patient-specific tolerance ranges before packaging.
The factory uses medical-grade silicone, latex-free elastic straps, and hypoallergenic adhesives that undergo biocompatibility testing to minimize skin irritation during prolonged wear.
A controlled environment prevents particulate contamination on the wound-contact surface, which lowers infection risk after transradial catheterization and supports faster recovery.
Each lot is assigned a unique digital batch record that tracks resin lots, mold cavity numbers, assembly operators, and sterilization cycles, enabling rapid recall if ever needed.
Devices are placed on anatomically designed forearm simulators that replicate different wrist sizes, tissue compliance, and movement to verify stability and pressure distribution over 24 hours.
Yes, tooling can be adapted for pediatric, elderly, or obese patients by adjusting strap length, curvature, and inflation volume while keeping the same safety validation protocols.
Production data is reviewed weekly by cross-functional teams, and small-batch pilot runs test ergonomic or material changes before scaling, ensuring safety is never sacrificed for efficiency.
Conclusion
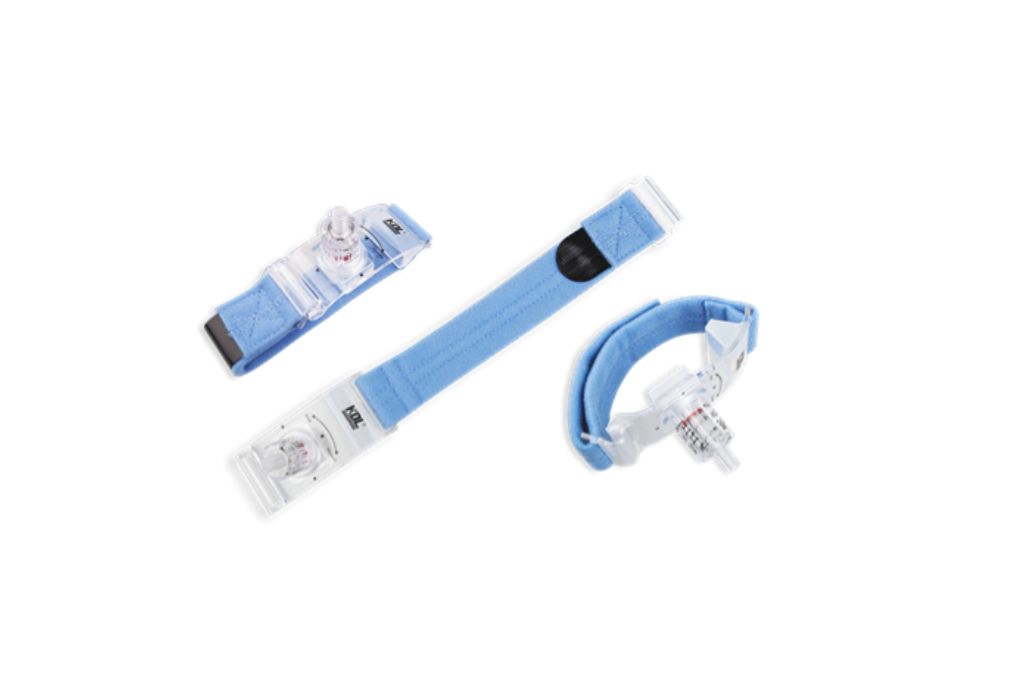
Inside the radial artery compression device factory, every detail is engineered around one fragile reality: the radial artery is only a few millimeters wide, and a poorly molded cuff can spell disaster. Our molding process holds tolerances at the micron level, because a seam or ridge invisible to the eye can still bruise or occlude. This same obsession carries into the sterile zone, where technicians work in laminar flow hoods and every tool is tracked. We do not treat sterility as a checkbox; we treat it as the moment precision meets a patient's open wound. From raw polymer extrusion to final pouch sealing, there are no shortcuts—each lot is traceable, each batch is quarantined until it passes.
What sets our factory apart is not just the machinery but the philosophy behind the pressure curve. We mapped hundreds of nurse-applied compressions to replicate a human touch, avoiding both ischemic injury and rebleeding. Then, before any device ships, it faces a fail-safe battery: each inflatable bladder is pressurized beyond clinical limits and submerged to flag even a microscopic leak. Finally, every unit carries a digital passport—a scannable record of its molding parameters, sterilization cycle, and test results—so the cath lab team sees exactly what we saw. That transparency is not marketing; it is the only honest way to build a device meant to sit on a beating artery.
Contact Us
Contact Person: Jeffrey
Email: [email protected]
Tel/WhatsApp: 86-0633-2230056
Website: https://www.sd-intmedical.com