OEM Laser Cutting Machine Selection Tips for Growing Manufacturers
2026-09-25
Scaling production without the right laser cutting partner can quietly drain your margins. Most growing manufacturers focus on price per watt and miss the real bottlenecks that surface weeks after installation. HUNSONE has spent years working beside OEMs at this exact growth stage, and the selection pitfalls we've documented are rarely mentioned in spec sheets. Here's what actually separates a machine that scales with you from one that stalls your expansion.
Match the Machine to Your Daily Material Mix, Not the Demo
A live demo shows you one clean stream at a time. Your Tuesday afternoon, on the other hand, is a tangled pile of stretch wrap, dirty OCC, a stray pallet, and maybe a chunk of purge the operator forgot to mention. Machines that shine on a single, uniform input often choke on the mixed reality of a working dock or sorting line.
Before you sign off on a rotor diameter or a bed knife count, track what actually crosses your infeed for two weeks. Not the ideal bale, not the showcase sample—the real average. If the daily blend is 60% film and 40% rigid plastic, the machine needs to chew that ratio without constant babysitting. If it eats a lot of thin, abrasive material, look for aggressive feeding geometry and wear parts you can swap without pulling the whole assembly.
Talking to operators helps more than watching a polished clip. Ask what jams, what they bypass, and what they wish the last machine had handled. Then spec for the ugliest hour of your week, not the prettiest one of the demo reel.
Look Beyond Kilowatts to Cutting Speed at the Thickness You Use
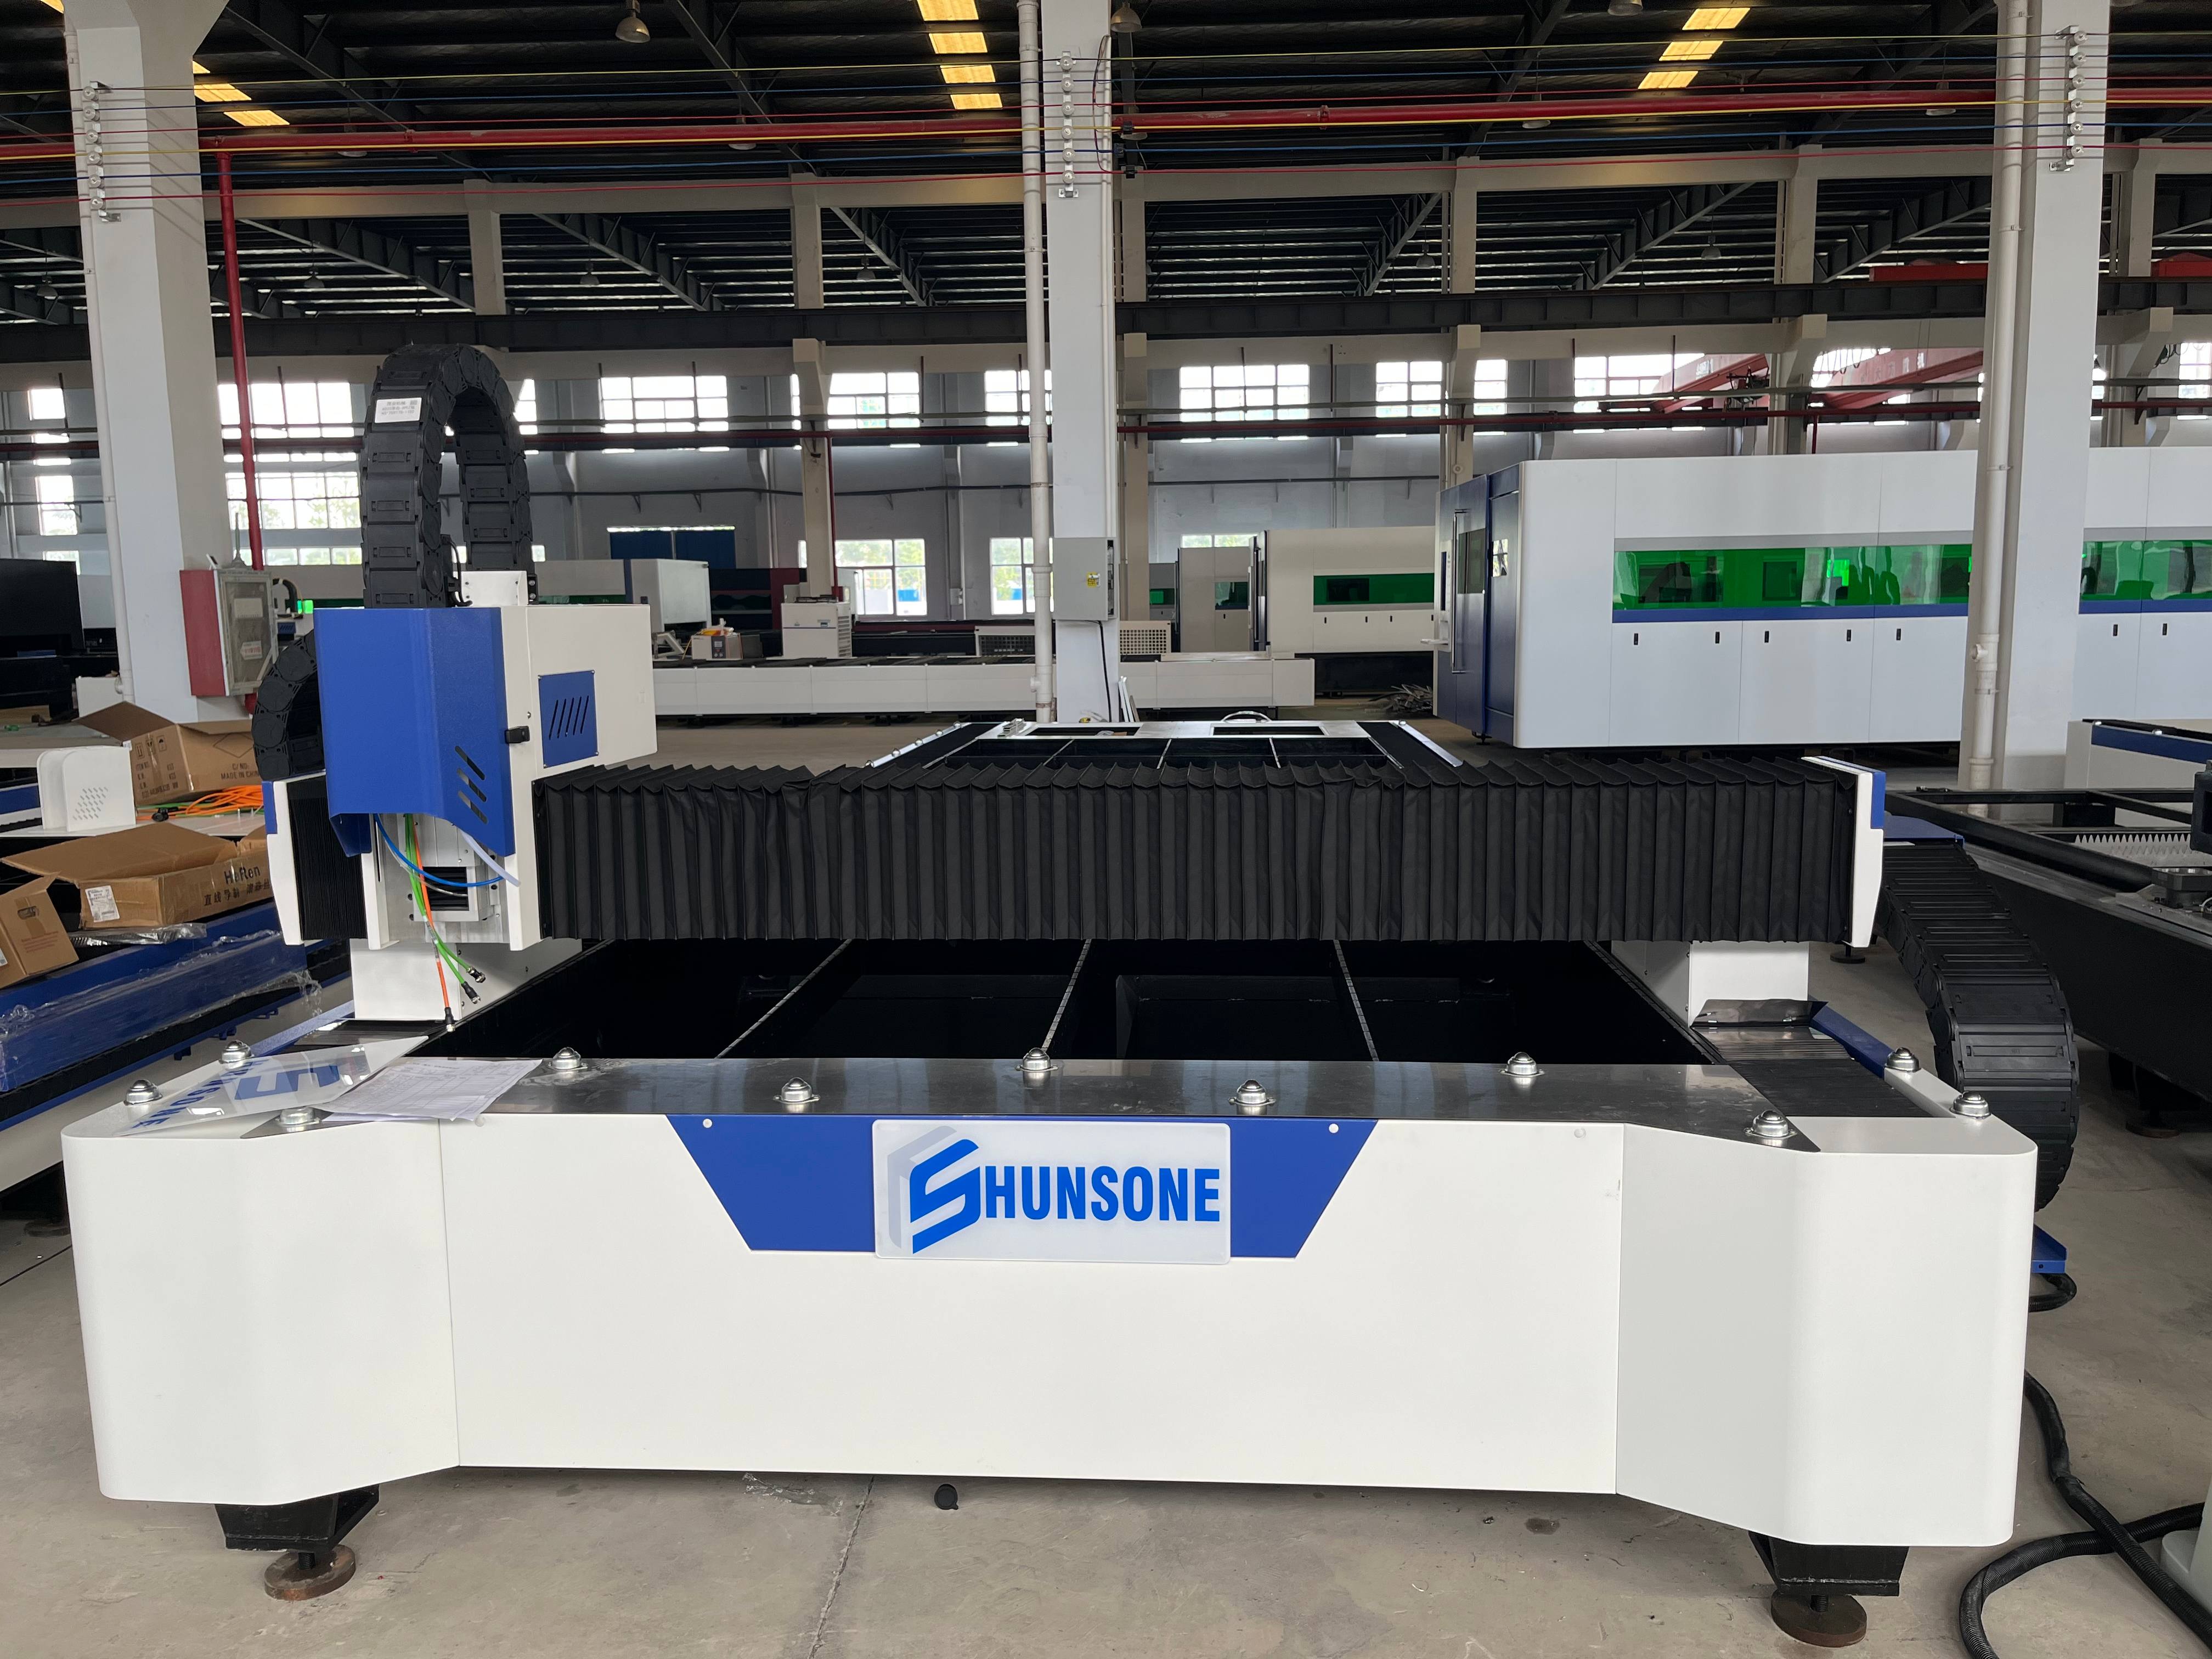
Most buyers fixate on laser wattage when choosing a cutting machine, but raw power rarely tells the full story. A 6kW source may slice through 10mm mild steel faster than a 4kW unit, yet on 3mm stainless the gap often narrows to a few seconds. The real question is what thickness you actually run day after day — because that’s where cutting speed, assist gas flow, and beam quality determine your true throughput, not the number on the nameplate.
At thin gauges, acceleration and piercing dynamics often outweigh nominal kilowatts. A well-tuned 3kW machine with a fast piercing routine can outpace a poorly optimized 6kW system on 1.5mm aluminum, simply because it spends less time starting each cut. Meanwhile, at 20mm carbon steel, the higher power finally pays off — but only if your lens, nozzle, and focal position are dialed in for that specific thickness. Blanket wattage comparisons ignore these operational realities.
So instead of asking “how many kilowatts,” ask “what’s the cutting speed at the thickness I use most?” Request sample cuts on your own material, time the full cycle including pierce and traverse, and compare gas consumption per part. That’s the metric that shows up on your production schedule — and your bottom line.
Count Consumables and Unplanned Downtime as Part of the Price
The real cost of running equipment rarely matches the sticker price. While the initial purchase figure captures attention, it overlooks the ongoing drain from consumables and the hidden toll of unexpected stoppages. A machine that demands frequent blade replacements or specialty lubricants quietly inflates its lifetime expense. Similarly, unplanned downtime—whether from a snapped belt, a failed sensor, or a jammed feed mechanism—steals productive hours and forces reactive maintenance. Treating these factors as integral to the price, rather than incidental afterthoughts, shifts the evaluation toward total operational burden.
Savvy buyers learn to back-calculate these variables into a comparable figure. A cheaper unit with higher consumable usage and a track record of sporadic failures may end up far more expensive than a pricier alternative built with durable, readily available parts. The math doesn't need to be perfect; even rough estimates of downtime frequency and consumable spend can reveal dramatic differences. When you fold these costs into the purchase decision, the "bargain" that halts production twice a month no longer looks so appealing.
This mindset also reshapes negotiation and design priorities. Instead of haggling over a few percentage points off the invoice, discussions can focus on guaranteed consumable lifespans, service response times, or modular components that reduce repair complexity. By making unplanned downtime and consumable burn part of the quoted price, both buyers and suppliers are pushed toward equipment that keeps running—not just equipment that was cheap on day one.
Check That the Control Software Talks to Your Current Design Tools
Before committing to a new control software stack, sit down with the tools your team already lives in every day. Are you driving models from Rhino, sketching in Fusion, or juggling assemblies in SolidWorks? The real test is whether the software can read your native files without a messy round-trip through yet another format. If your engineers have to export, clean, and re-import just to get a toolpath, that friction will show up in every project timeline.
Look for plugins or direct integrations that feel like a natural extension of the CAD environment, not an afterthought. A good control package should let you pull dimensions, constraints, and even design history straight into the CAM setup. When the software understands parametric changes automatically, a late-stage tweak doesn't become a manual rework marathon. That kind of tight loop keeps designers and machinists from drifting into separate worlds.
Also pay attention to version compatibility and how updates are handled. Nothing stalls a production floor faster than discovering the latest CAD service pack broke your post processor. Ask about real-world test cases with your exact design tools, and if possible, run a pilot project with a simple part before rolling it out broadly. The goal is a workflow where the control software quietly fits in, not one that demands you rebuild your design process around it.
Ask for a Service Map, Not a Service Promise
A promise like "we’ll always be there when you need us" sounds reassuring but tells you nothing about how the work actually gets done. That’s why you push for a service map instead. Ask the provider to walk you through each stage of delivery: who receives the first request, what systems they touch, where handoffs happen between teams, and which triggers escalate an issue. The map should show not just the happy path but the detours for complaints, delays, and unexpected failures.
When someone can draw that map without hesitation, you’re seeing operational memory, not marketing copy. You learn whether support tickets sit in a shared inbox for two days or route automatically to a named owner with a time stamp. You can spot bottlenecks like a single person being the bottleneck for approvals, or a vendor subcontracted for a critical step that the main provider doesn’t control. A real map exposes those seams.
Most importantly, the request itself separates serious operators from those who only sell confidence. A team that has never mapped its own service flow will stall, give vague answers, or switch back to promises. A team that hands you a clear, current map—or offers to build one with you—shows they treat service as a design problem, not a slogan. That’s the kind of partner worth signing with.
Bring Your Own Files for a Test Run Before Signing
You wouldn't buy a pair of shoes without trying them on, so why commit to a software subscription before seeing how it handles your actual files? Most platforms let you poke around with sample data, but those tidy examples rarely reflect the messy reality of your own spreadsheets, PDFs, or image folders. Upload a few real documents—especially the oddball ones with weird formatting or embedded objects—and watch what happens. If the tool chokes on a file you use every week, that's a red flag you won't find in any polished demo.
A test run doesn't need to be complicated. Grab three or four files you already have open on your desktop: a contract draft, a batch of photos from last month, maybe a CSV export from your accounting software. Run them through the upload flow, the conversion step, or whatever core action the service promises. Pay attention to small friction points—does it preserve fonts? Does it rename files unexpectedly? Does it time out on larger uploads? These details matter more than a flashy interface when you're staring down a yearly plan.
Once you've seen your own content move through the pipeline, you'll have a much clearer sense of whether the subscription earns its price. You might even discover that the free tier already covers your needs, or that a competitor handles your file types with less hassle. Either way, you've made a decision based on evidence, not a sales pitch. And if the trial period expires before you finish testing? Most tools will happily extend it if you ask—just be honest that you're comparing options.
FAQ
Focus on the real bottlenecks in your current workflow. If you're losing time on thick stainless, prioritize a stable cutting head and reliable assist gas delivery over raw wattage. Also check whether the OEM offers modular upgrades, because your needs will shift as orders grow.
Don't just go by maximum wattage. Map out the thickest and thinnest materials you run weekly. For mild steel up to 6mm, 1.5–2kW is usually enough; for 10mm+ stainless or aluminum, look at 3kW or higher. But also pay attention to beam quality and focal length—cheap high-power tubes can ruin edge finish on thin sheets.
Unless your production is very standard, a custom OEM build often pays off. You can get a gantry sized for your sheet stock, a specific nozzle setup, or a control interface that matches your team's workflow. Just make sure the OEM documents every modification, or you'll be stuck troubleshooting a one-off machine alone.
Chiller maintenance, lens replacements, and exhaust filtration are the usual surprises. Some suppliers quote only the bare frame, then you find out the fume extractor isn't included, or the chiller is undersized for continuous shifts. Ask for a turnkey quote that includes installation, training, and a spare parts kit for the first six months.
Software can make or break daily output. If your team already uses SolidWorks or AutoCAD, check that the OEM's control software imports DXF or DWG cleanly, and that nesting is included. A machine with a clunky proprietary interface may save money upfront but cost hours every week in manual workarounds.
Expect weekly cleaning of the protective lens and rails, monthly checks on the chiller coolant and filters, and periodic beam alignment. If you run reflective materials like aluminum or copper, you'll also need a robust autofocus and possibly a protective window upgrade. Budget for a maintenance contract if the OEM is not local.
It's tempting to buy the biggest machine now, but oversized laser sources can be inefficient for thin sheet work and harder to justify. Look for a platform with modular power—start at 2kW and add later if the frame and motion system allow it. That way you keep initial costs down without painting yourself into a corner.
Ask about real-world cutting speed on your specific materials, not just the brochure numbers. Request a sample cut or video demo. Also ask about lead time for spare parts, remote diagnostics, and whether they have local service engineers. If the OEM hesitates to share these details, keep looking.
Conclusion
Growing manufacturers often pick an OEM laser cutter after watching a flashy demo, only to discover the machine struggles with the day-to-day stack of materials already queued on the floor. Before talking to a vendor, pull your last three months of job tickets and group them by material type, thickness, and edge-quality requirements. A machine that blazes through 20-gauge stainless but crawls on quarter-inch mild steel might be exactly wrong for your mix. So match the equipment to the actual daily workload, not the sample part in the showroom.
Power ratings are likewise a poor proxy for productivity. Two 6kW lasers can differ dramatically in cutting speed at the thickness you actually run because of beam delivery, assist gas dynamics, and motion control. Ask for time studies on your own material stack, not the vendor's cherry-picked coupon. Then add up the true operating cost: nozzle replacements, lens protection windows, filter media, and the lost hours from unplanned stops. A cheaper machine with frequent consumable changes and a thin service network can cost far more over two years than a pricier one that simply keeps cutting. Make sure the control software imports your existing CAD/CAM files without a translation mess, and press the vendor for a concrete service map—names of local technicians, typical response windows, spare parts stocked in your region. Finally, bring three or four of your hardest files and run them yourself. If the vendor hesitates, that hesitation is the most useful specification you will get.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/