OEM Hybrid Servo Press Brake Delivers Unmatched Precision for Complex Bending Tasks
2026-10-05
When precision is non-negotiable and complex bending tasks demand perfection, standard press brakes often fall short. The OEM Hybrid Servo Press Brake from HUNSONE redefines what’s possible, blending hybrid drive technology with servo accuracy to tackle the most intricate geometries effortlessly. Discover how this machine transforms challenging bends into repeatable, high-quality results.
Hybrid Servo Motion Without the Marketing Hype
Most motion control vendors throw around 'hybrid servo' as if it is a magic blend of stepper simplicity and servo performance. Dig into the hardware, and what you actually get is a closed-loop step motor: a two-phase stepper paired with an encoder and a drive that checks position instead of blindly sending pulses. That single change eliminates lost steps under normal load variation, but it does not transform the motor into a high-bandwidth servo.
Torque still falls off as speed increases because the drive is pushing current through the same windings. Below roughly 800 to 1000 rpm, the feedback loop catches missed steps and applies a short burst of extra current to recover. Above that, the back-EMF leaves little voltage headroom, so correction ability fades. If your application runs mostly at low speed with occasional overloads, this setup works well. If the motion profile demands constant high rpm or rapid acceleration, a conventional AC servo with a properly sized amplifier will outperform it.
The practical appeal is not raw performance—it is that you keep pulse-and-direction control and avoid the tuning complexity of a full servo drive. Wiring stays simple, and commissioning takes less time. But set expectations accordingly: you get closed-loop position verification and useful disturbance rejection, not servo-grade dynamic response. Treat it as a smarter stepper, not a cheaper servo, and it fits a lot of real-world tasks without the inflated claims.
Complex Bends That Used to Require Multiple Setups
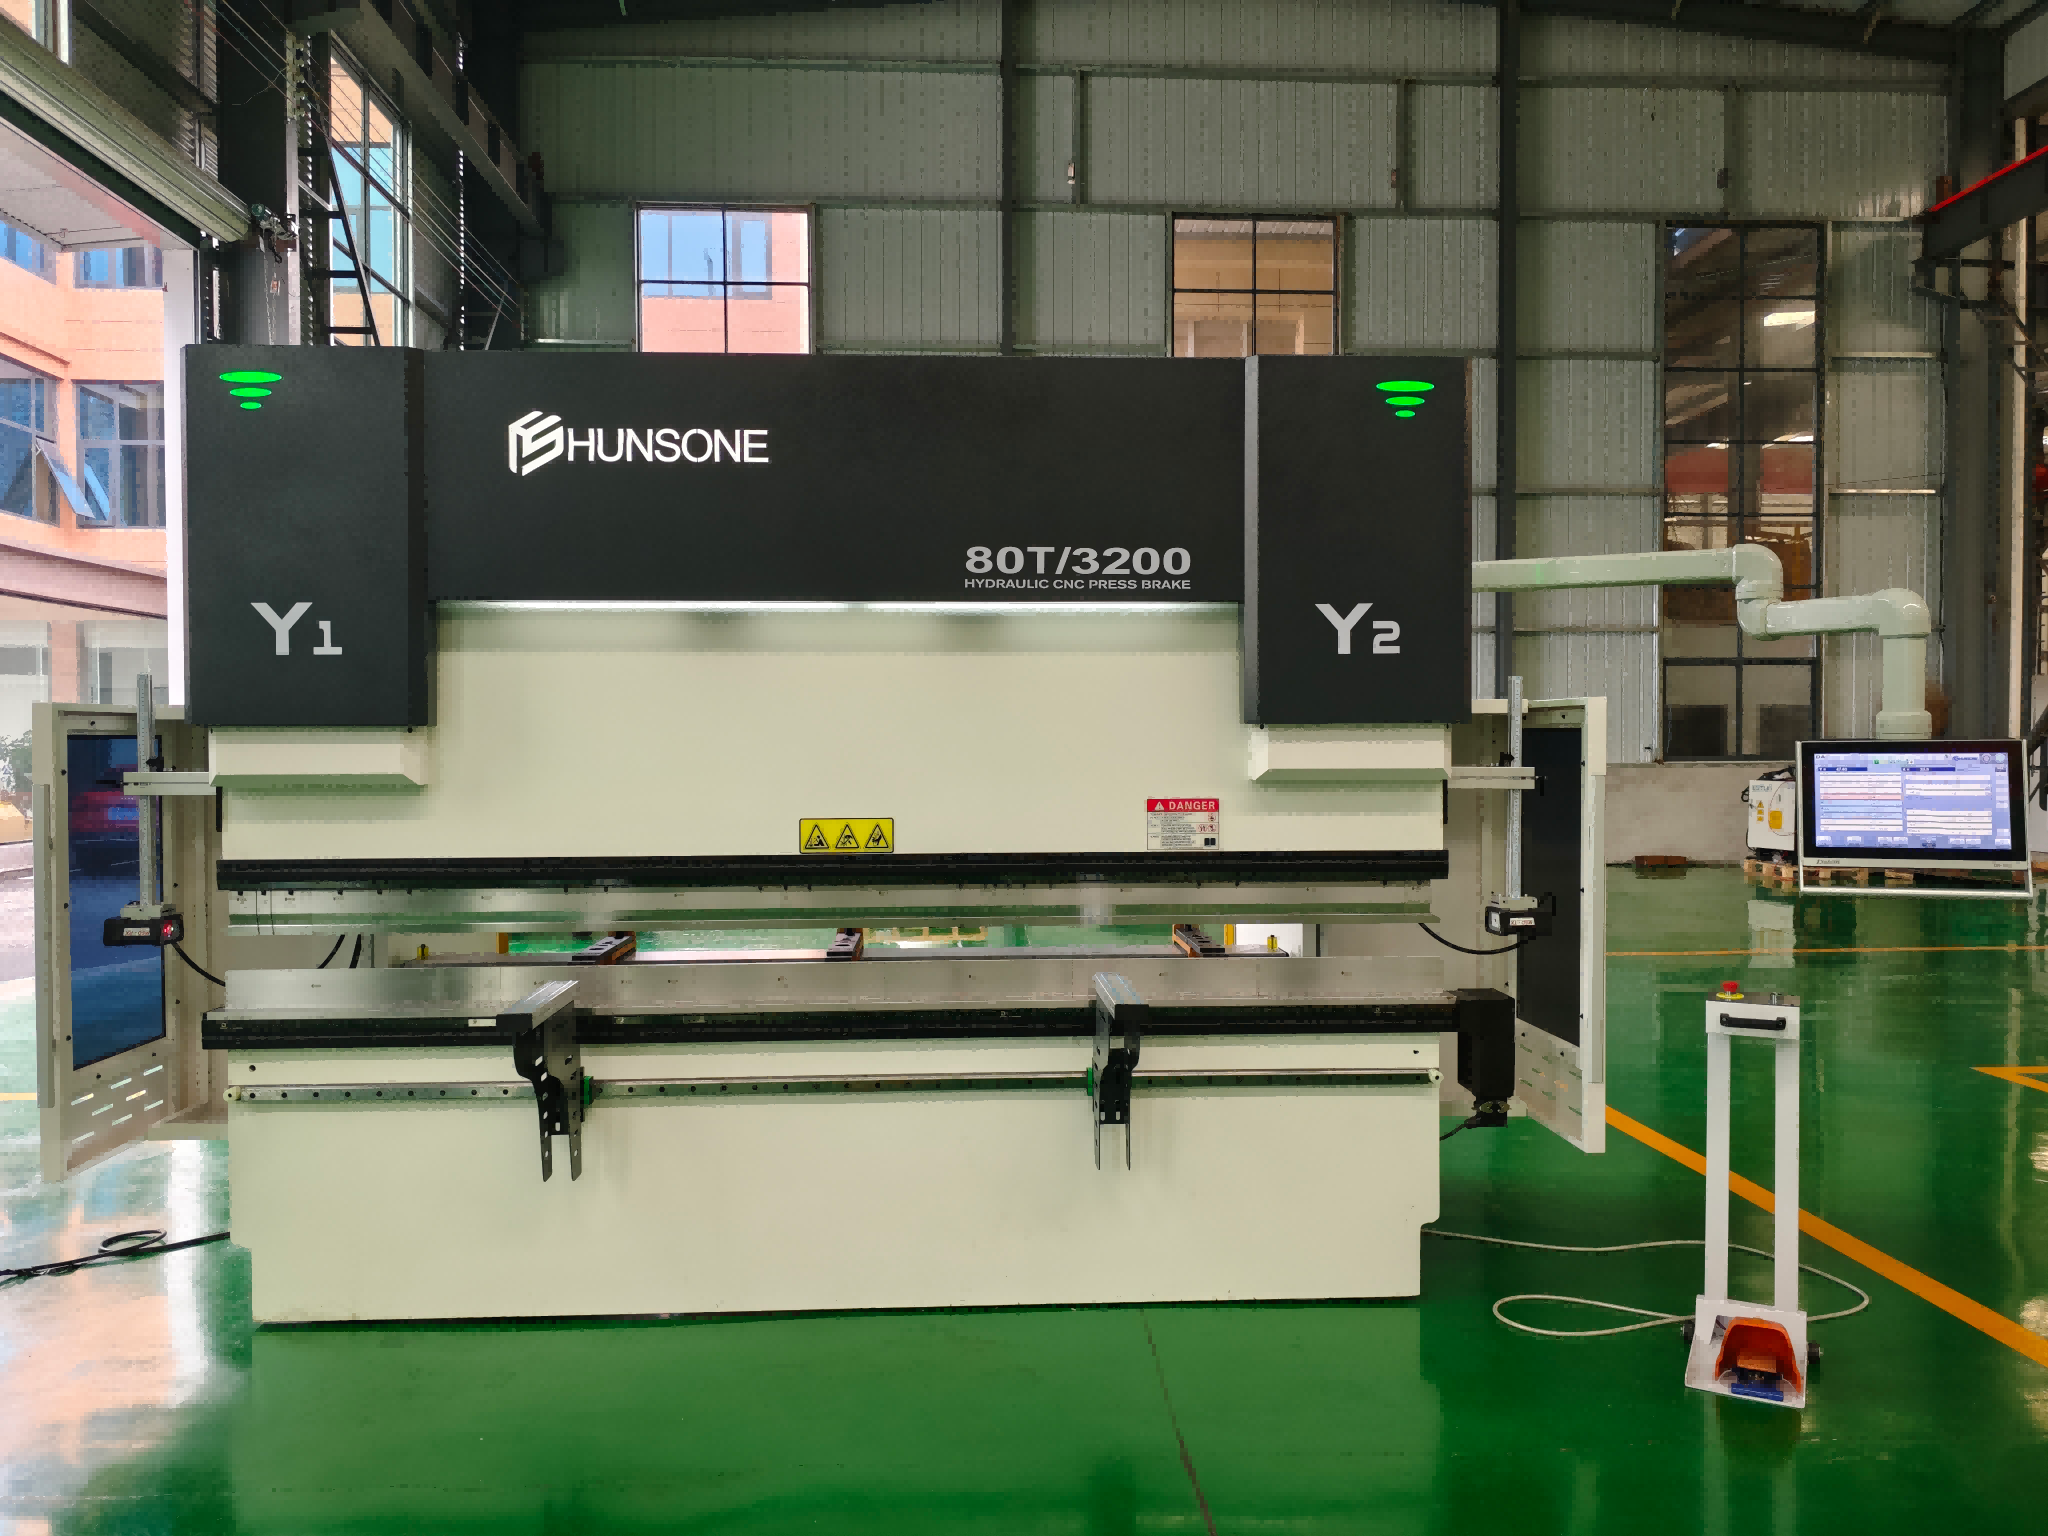
Older press brakes often forced shops to break a single complex part into several stages. A bracket with a deep offset, a reverse flange, and varied radii might need three or four different tool stations, each with its own backgauge position and bend sequence. Operators spent time repositioning, checking angles, and hoping nothing shifted between setups. Tolerances stacked up quickly because every re-clamping introduced a fresh chance for misalignment.
Modern CNC press brakes and automated bending cells handle what used to be multi-setup headaches in one clamping. Multi-axis backgauges move the part without manual intervention, while adaptive crowning and real-time angle measurement keep bends consistent across the full length. Tooling libraries and offline programming also let the controller plan the sequence automatically, so a complex profile with reverse bends and tight radii isn't treated as a series of separate jobs anymore.
The payoff shows up most in low-volume, high-mix work. Instead of cutting extra blanks to account for scrap from setup errors, a shop can run one piece through and get a usable part the first time. That reduces work-in-process and eliminates the need to match marks or recheck fixtures between operations. Complex bends that once meant hours of staging now come off the machine in minutes, with repeatability that manual repositioning could never match.
OEM Customization That Actually Fits Your Workflow
Most OEM customization stops at swapping logos and picking a color scheme. That might look nice in a screenshot, but it does nothing for the way your team actually moves through tasks. Real fit starts with how orders get logged, how inventory flags trigger reorders, and how production updates reach the people who need them. It means letting you define those steps, not forcing you to adapt to a fixed sequence baked in by someone who has never seen your floor.
A custom workflow should feel like it was already part of your toolkit. That happens when the OEM layer exposes the same hooks, scripts, and data fields your internal tools rely on. Instead of learning a new interface to bridge the gap, you connect what you already use — whether it's a barcode scanner, a spreadsheet tracker, or a homegrown ERP module — and the OEM layer quietly carries the load. No extra clicks, no duplicate entry, no "workaround mode" that everyone secretly hates.
Workflows change. Suppliers change, compliance rules shift, and the person who used to approve orders leaves. An OEM setup that fits today may not fit six months from now unless it's built to evolve. Look for a customization model where you can adjust prompts, reorder steps, or add conditional branches without filing a support ticket. Then the system adapts to your workflow, not the other way around.
The Precision Difference You Can Measure in Microns
In industries where a single human hair is roughly 70 microns wide, holding tolerances to just a few microns changes everything. This isn't abstract talk about quality; it's the difference between a bearing that spins quietly for a decade and one that seizes after a year. Manufacturers chasing that level of control need measurement systems that don't just report numbers, but reveal exactly where a process begins to drift before parts ever leave the line.
The real test often shows up at the edge of what's measurable. A three-micron variation on a sealing surface can decide whether a fuel injector holds pressure at 200 bar or leaks from day one. That's why modern inspection goes far beyond pass or fail. It maps surface variation, tracks tool wear, and gives machinists a concrete reason to adjust offsets while the deviation is still small enough to correct.
More than anything, micron-level precision is rarely the result of one heroic machine. It comes from tightly controlled environments, thermal compensation, and routines that make repeatability almost boring. When measurement uncertainty drops well below the feature tolerance, the conversation moves from "can we make it?" to "can we make it again tomorrow at 2 p.m.?" That kind of consistency is what customers feel every day, even if they never see the numbers behind it.
Lower Energy Draw, Same Shop-Floor Muscle
Most plant managers have learned the hard way that chasing lower utility bills often means accepting a drop in torque, speed, or cycle time. That trade-off disappears when you look at the latest generation of synchronous reluctance motors paired with smart drives. They pull significantly fewer amps during continuous duty, yet they still deliver the abrupt starts, rapid reversals, and sustained loads that keep a stamping line or a machining center from falling behind.
The real difference shows up in the fine print of your power meter. Instead of bleeding reactive power as waste heat, these systems keep the magnetic flux tightly aligned with the rotor position. The result is that a 15 kW frame can often replace a 22 kW induction unit without any drop in breakaway torque or holding accuracy. Maintenance crews notice the change in the control cabinet too—cooler drives, fewer nuisance trips, and no need to oversize contactors just to survive inrush spikes.
On the floor, that translates to the same aggressive feed rates and chip loads your operators are used to, whether they're pushing aluminum through a gantry mill or running a conveyor under heavy accumulation. The energy savings don't announce themselves with reduced performance; they show up quietly on the monthly invoice while the spindles keep humming at full song.
What Changes When Rework Rates Drop to Nearly Zero
When rework stops being a routine part of production, the most immediate shift is in time. Teams no longer reserve buffer days for fixing what should have been right the first time, so lead times compress and delivery dates become dependable rather than aspirational. That predictability quietly changes how customers perceive you—not through marketing, but through a track record that stops including exceptions.
Cost behavior also drifts away from the old assumption that quality improvements pay for themselves slowly. With near-zero rework, the hidden overhead of extra materials, inspection after the fact, and overtime to correct errors simply evaporates. Managers find they can redeploy those resources into preventive maintenance, better tooling, or even new product trials—activities that were previously squeezed out by the constant pressure to fix yesterday's mistakes.
Perhaps the least expected change is cultural. When operators and engineers stop treating rework as a normal part of the job, the conversation shifts from blame to prevention. People begin asking why a defect almost happened instead of who let it slip through. That subtle reframing builds a deeper sense of ownership, and over time, the line between production and quality blurs until they become the same activity.
FAQ
The hybrid servo drive pairs a servo motor with a hydraulic pump that only runs when force is needed, so ram movement stays tightly controlled without the lag or overshoot common in fully hydraulic machines. This gives you smoother acceleration and deceleration through the bend cycle, which matters a lot when you're working with tight radii or parts that have multiple bends close together.
Accuracy comes from a few layers working together: linear encoders feed real-time ram position back to the controller, the frame is thermally compensated to reduce drift as the shop warms up, and the crowning system adjusts automatically based on the load profile. That combination keeps repeatability within a few microns even after hundreds of cycles.
Yes, but it depends on the tooling and material condition. The servo-driven ram allows very slow, controlled approach speeds near the pinch point, which reduces the risk of cracking in high-strength steel or aluminum. Pair it with the right die opening and a precision-ground punch, and you can hold a tight inside radius without overstressing the material.
You can specify bed length, tonnage, open height, stroke, and backgauge travel to match your product line. Beyond that, we offer custom tooling holders, automated loading interfaces, robotic bending cells, and bespoke control software that can store part recipes with all bend parameters baked in.
Because the servo pump idles when the ram is not moving, energy use drops by roughly 40 to 60 percent compared to a fixed-displacement hydraulic system. Noise also falls significantly, often below 70 dBA during standby, which makes the machine more comfortable to work around and easier on the shop floor.
For complex parts, a segmented upper punch and multi-V lower die give you flexibility, while a CNC backgauge with at least four axes lets you position stops independently for asymmetric profiles. Adding a front support arm or sheet follower helps keep large or thin blanks from sagging during the bend sequence.
Most operators pick it up within a couple of days because the interface is built around a graphical bend simulation rather than raw G-code. You set the target angle, material thickness, and tooling layout, and the controller calculates the punch depth and backgauge position. There is still a manual mode for fine-tuning, but the learning curve is much shorter than you'd expect.
A monthly check of the hydraulic oil level and filter condition is the big one, along with greasing the ram guides every 40 to 60 operating hours. We also recommend a yearly laser alignment check on the ram and backgauge, plus a servo drive diagnostic to catch any encoder drift before it affects bend accuracy.
Conclusion
Hybrid servo press brakes have long been sold on buzzwords, but the real story here is simpler: this OEM machine bends complex parts with a repeatability you can actually verify. The hybrid servo motion isn’t about flashy claims—it’s about holding position within microns while ramping force only when needed. Cutting out the constant full-power hydraulic draw means the same shop-floor muscle comes with a noticeably lower energy bill. Jobs that used to demand multiple setups, shims, and trial pieces now run in a single handling because the control adapts bend angles on the fly, compensating for springback and material variance before they become scrap.
That precision changes how a shop operates. When rework rates drop to nearly zero, you stop budgeting hours for sorting and touch-ups, and start scheduling more jobs through the same machine. The OEM customization matters here because it’s not a one-size-fits-all interface—it’s built around your tooling, your part families, and your operators’ habits. Instead of forcing your workflow around the machine, the control layout, backgauge logic, and even safety zones can be tailored. The result is a press brake that doesn’t just hit tight numbers in a demo; it keeps hitting them on the third shift, with less power, fewer adjustments, and far fewer rejected parts.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/