Bulk Motor Magnet Essentials: A Practical Guide for Manufacturers
2026-08-16
Every motor manufacturer knows the frustration of sourcing magnets that meet torque specs but fail on consistency—one batch perfect, the next riddled with cracks or off-spec coercivity. Bulk procurement only amplifies the pain. This practical guide cuts through supplier jargon to give you a no-nonsense checklist for evaluating bulk motor magnets, from grain size distribution to plating adhesion under thermal cycling. Along the way, you’ll see why DAWA has become the quiet standard for production teams that can’t afford rework.
Never Trust a Data Sheet: Field Checks That Expose Underperforming Magnets
A data sheet might promise a surface field of 5,200 gauss and a pull force of 12 pounds, but those numbers are usually measured under lab-perfect conditions. In the field, magnets get hot, get chipped, or come off a production line with uneven magnetization. Before you trust a critical holding or sensing application, do a quick pull test with a calibrated spring scale against a clean, flat steel plate. You'll often find that a batch of “N52” magnets behaves more like N42 once they've been sitting in a hot enclosure for a week.
Another revealing check is to move a gaussmeter probe across the pole face at a fixed working distance. Look for dead spots or a lopsided field profile—those are signs of poor magnetization or internal cracks. Also slide a piece of thin paper between magnet and keeper; if it snags on coating blisters, that's a future corrosion point. These checks take minutes but catch the difference between a magnet that meets spec on paper and one that actually works where it's installed.
The Real Cost of Cheap Neodymium: Where Bulk Buyers Lose Money
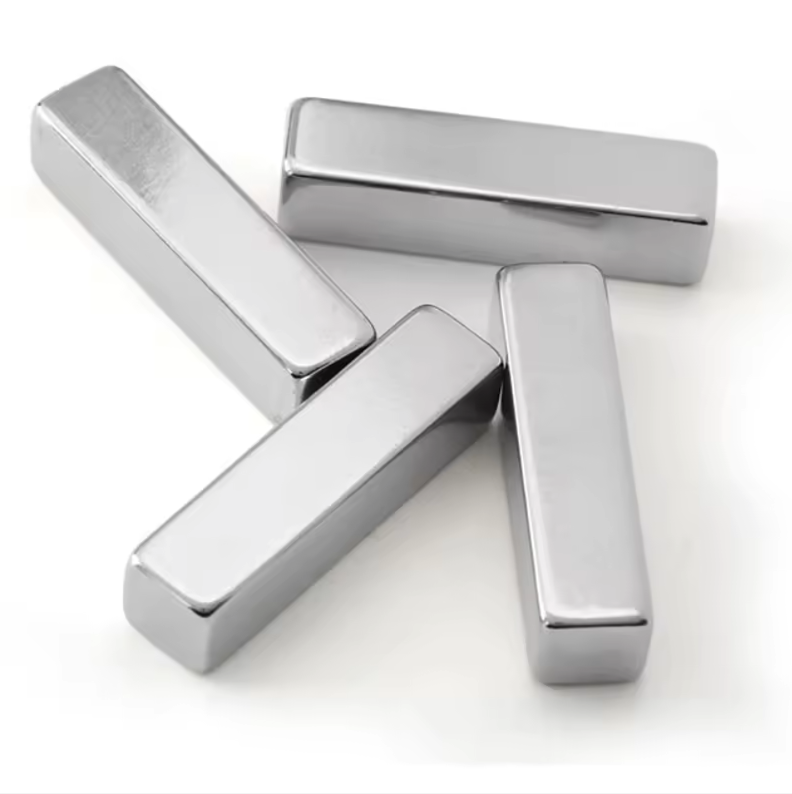
Sourcing neodymium at rock-bottom prices feels like a win on paper, but the true expense rarely shows up on the initial invoice. Bulk buyers often discover that substandard magnets fail tolerance tests, forcing rework or wholesale rejection of entire production runs. The hidden cost isn't just the wasted material—it's the lost machine hours, delayed shipments, and the slow erosion of trust with your own customers.
Another silent drain comes from inconsistent magnetic performance. Cheap neodymium frequently suffers from uneven coercivity and poor temperature stability. When a batch passes a simple pull test but degrades under load or heat, you're not saving money—you're gambling with warranty claims and field failures. Smart procurement teams know that a slightly higher per-unit price from a certified supplier almost always beats the compounding cost of field replacements.
Finally, there's the procurement overhead nobody budgets for: extra incoming inspections, supplier audits, and the constant re-quoting when a low-cost vendor can't meet delivery dates. Every hour your engineers spend sorting marginal material is an hour not spent on product improvement. In the rare-earth market, price without reliability is just a down payment on future losses.
Tolerance Stacking: The Silent Killer of Motor Assembly Lines
Most motor assembly lines still treat tolerance as a per-part inspection problem. A shaft measures 10.00 mm instead of 9.98 mm, a housing bore comes in at 20.01 mm, and each part passes. But once those parts are pressed together, the tiny deviations stack up. The result is a rotor that sits off-center, uneven air gaps, and bearings that get preloaded without anyone noticing. The line keeps running because every single component is within spec, yet the finished motor fails vibration or noise tests downstream. That is the quiet nature of tolerance stacking—it hides inside individual measurements and only shows up after assembly.
There are two ways engineers usually look at this. Worst-case analysis assumes every dimension sits at its extreme limit, which almost never happens but makes the math simple. Statistical tolerance analysis, like root-sum-square, is closer to reality because it accounts for the probability that not all parts will drift the same way at the same time. The problem is that many assembly lines rely on incoming part inspection rather than stack-up simulation. A supplier can ship hundreds of housings that are all within print, but if the bore is consistently on the low side and the bearing ODs are consistently on the high side, the interference fit becomes a press nightmare. No single part is bad; the combination is.
Fixing it means moving upstream. Instead of reacting to end-of-line failures, teams have to model the stack before tooling is even cut. That might mean adjusting nominal dimensions, tightening tolerance bands on a few critical features, or adding a flexible assembly step like selective fitting. Some plants use in-process gauging to measure actual mating parts and pair them on the fly. It costs more upfront, but it beats scrapping finished motors or, worse, shipping units that wear out early. Tolerance stacking gets called a silent killer because the assembly line can run for weeks before a batch of marginal builds finally tips over into functional failure. By then, the root cause is buried under thousands of good parts.
Coating Failures You Won't See Until It's Too Late
A coating can look flawless on the surface while quietly breaking down underneath. The real trouble starts at the interface—microscopic adhesion loss, osmotic blistering, or underfilm corrosion that never shows up in a visual check. By the time the first rust stain or peeling edge appears, the damage has often spread far beyond what you can see.
Some of the worst failures hide in places nobody inspects until a shutdown: behind flanges, inside tank corners, under insulation, or on the back side of structural members. Moisture wicks into these areas, and the coating fails from the back out. You won't notice it during routine walk-downs, but the substrate is losing thickness every day.
The most deceptive part is that many coatings fail gradually, then suddenly. Tiny cracks give salt water a path to the steel, but the surface still feels hard and intact. One thermal cycle or mechanical stress later, whole sections delaminate. Without destructive testing or advanced NDT, you're flying blind until the coating gives out completely.
How to Read a Supplier Audit Like a Factory Floor Veteran
Veterans skip the executive summary and thumb straight to the nonconformance section, but not to count issues. They look for patterns that repeat across shifts, lines, or visits. A single miss is just noise; the same torque drift on line three across three consecutive audits is a failure nobody has owned. They also read between the lines when an auditor downgrades something serious to “observation” because the supplier asked nicely.
The corrective action log tells you more than any score. A floor veteran checks how many CAPAs passed their due date, how many were closed with “retrained operators” as the only fix, and how many reopened within ninety days. That ratio separates suppliers who fix root causes from those who fill out paperwork. If the same issue appears on the next audit with a new date, the system is performing, not improving.
Then they flip to the evidence. Photos that only show brightly lit, empty aisles are a red flag. Look at the Cpk values: if every process capability number is conveniently above 1.67, either the supplier chose the best runs or the measurement method is asleep. Veterans trust what is missing as much as what is included, and they know a clean audit with no findings often means the auditor never left the conference room.
Stocking Up Without Getting Stuck: Smart Inventory Plays for Bulk Magnets
For bulk magnets, the line between a healthy buffer and a cash-draining shelf full of oxidized stock is thinner than most people think. Instead of relying on a single average monthly volume, split your SKUs into two pools: the high-turnover standard sizes that you can reorder quickly, and the slower custom shapes where long lead times force you to hold more cover. For the first group, keep a dynamic safety stock fed by actual weekly demand rather than a fixed percentage. For the second, negotiate smaller batch shipments even if the unit price nudges up; paying a bit more per magnet beats watching your working capital sit in a corner while the plating starts to dull.
A smarter move is to break the vendor habit of trading price for volume. Many magnet suppliers will wave a lower per-piece rate if you commit to a large MOQ, but that often means six months of inventory for a product that may shift in specification or demand. Ask for staged deliveries against a single purchase order—same total quantity, but spread over quarterly or monthly drops. If your supplier balks, look into shared container space with a non-competing importer or a local distributor who can hold buffer stock for you. Remember that neodymium prices can swing hard, so locking in a long-term supply agreement with flexible release dates gives you coverage without the full financial exposure.
Finally, let the reorder point do the talking. Calculate it from actual lead-time variability plus a demand cushion, not from a guess. A simple formula—like maximum weekly usage times the supplier’s worst-case delivery week—can save you from both stockouts and accidental overbuying. Run a monthly aging report on your magnet inventory; anything sitting beyond ninety days without a matched order deserves a markdown or a repurposing plan. Warehousing bulk magnets isn’t free, and dead stock of magnetic assemblies can become a real headache when specs change. Keep your inventory lean where you can, deep where you must, and always tie every purchase back to a confirmed or strongly projected need.
FAQ
For most motor designs you'll compare N35 through N52, but the letter suffix after the number is just as critical. An N42SH can handle 150°C whereas standard N42 starts losing flux irreversibly above 80°C. Match the grade to your peak winding temperature, not just the room-temperature spec.
Request a pre-production sample run of 50 to 100 pieces and measure flux density, coating thickness, and dimensions across all of them. Ask for the supplier's process capability index and request third-party testing if anything falls outside agreed tolerances. Consistent demagnetization curves matter more than a single impressive data sheet.
Nickel-copper-nickel works for most indoor applications, but epoxy or parylene are better when you expect salt spray, humidity, or direct contact with cooling fluids. Zinc and aluminum IVD coatings offer a decent middle ground for cost and corrosion resistance, but adhesion under thermal cycling is what separates a reliable coating from one that flakes off after a few hundred hours.
Buy unmagnetized whenever possible. Magnetized parts attract ferrous debris, stick together, and can crack during automated handling. Magnetizing after assembly lets you control polarity orientation and avoid damage from repelling forces on the production line.
Near-net-shape forming like radial rings or arc segments eliminates most grinding and machining, which is where material loss and micro-cracks happen. Tooling costs more upfront, but a well-designed custom shape can cut scrap rates from 30 percent down to single digits and simplify rotor assembly.
Two coefficients matter: one for remanence (Br) and one for coercivity (Hcj). As temperature rises, both drop, but the coercivity loss is irreversible if you exceed the grade's maximum operating point. Choose a magnet whose Hcj rating leaves at least a 20 percent margin above your worst-case hot spot.
Use non-ferrous trays, individual spacers, and magnetically shielded containers to stop parts from slamming together. Add vapor-phase corrosion inhibitor bags inside sealed packaging if the shipment might sit in a humid port. Inspect for chipped edges upon arrival, since even small chips create nucleation sites for corrosion and flux loss.
Look at their scrap rate history, lead time consistency, and whether they warehouse buffer stock for you. Ask about their in-house testing lab and how they handle a delayed container or a rejected batch. A supplier who can provide detailed failure analysis and process adjustment within 48 hours is worth more than a cheaper quote that leaves you guessing.
Conclusion
Bulk motor magnet procurement is rarely as simple as matching a datasheet to a spec. Field checks matter because magnets that look perfect on paper often fall short under real operating conditions—flux density can drift, dimensional inconsistencies appear, and performance degrades once heat and load enter the picture. Cheap neodymium is another trap: lower-grade material or recycled feedstock may save money up front but quietly eats into margins through higher scrap rates, inconsistent pull strength, and premature field failures. On the assembly line, tolerance stacking turns tiny individual deviations into misaligned rotors, excessive vibration, and motors that fail final testing. Coatings add yet another layer of risk—pitting, blistering, or thin spots hidden beneath a visually smooth surface only show up weeks or months later as corrosion spreads inside the motor.
Supplier audits separate reliable partners from slick sales pitches when you read them like a floor veteran: look past the certificates and check how the factory actually controls sintering temperature, plating thickness, and lot-level traceability. A plant that cannot explain its raw material sourcing or show real batch data is a red flag no matter how polished the quote. Inventory strategy is the last piece—bulk buying can lock in price, but overstocking invites oxidation, demagnetization from poor storage, and cash tied up in slow-moving sizes. Smart buyers use tiered stock levels, climate-controlled warehousing, and first-in-first-out rotation. The manufacturers who combine rigorous incoming inspection, honest supplier evaluation, and disciplined inventory control are the ones who keep motor lines running without costly surprises.
Contact Us
Contact Person: Kelvin Lo
Email: [email protected]
Tel/WhatsApp: 0769-88561131
Website: https://dawamagnetic.com/